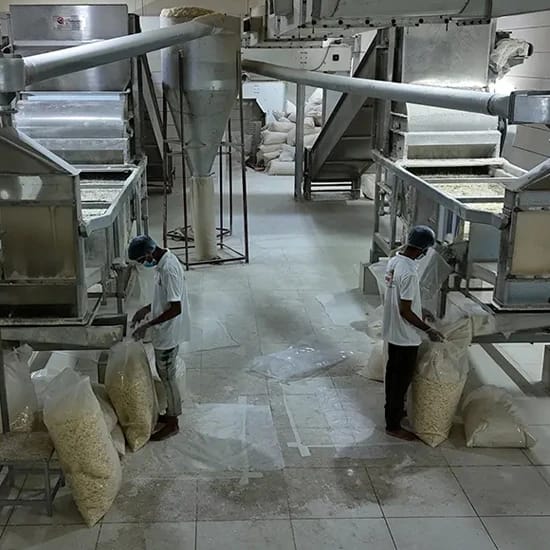
Hembird International Team
Our Journey

The Hembird Story

Founded in 2020, Hembird International started as a family-driven venture with a vision to share premium dehydrated products with the world. Guided by passion and commitment, we have grown into a trusted name in the global food industry—recognized for our uncompromising quality, reliability, and customer focus.

Our Vision

To become the most trusted global supplier of premium dehydrated food ingredients.

Our Mission

To deliver unmatched quality through strict quality control, continuous innovation, and a customer-first approach.

"At Hembird, we believe true success is built on relationships, not just business. For us, **every customer is family**—and this belief has shaped our journey since day one. With integrity, consistency, and care at the core of everything we do, we ensure our customers always receive products they can trust."
Our Guiding Principles

Building Global Food Solutions

MISSION
Mission Icon

Our Mission

To revolutionize Dehydrated exports through innovation, sustainability and uncompromising quality standards.

VISION
Vision Icon

Our Vision

To be the world's most trusted partner for premium Dehydrated ingredients across global markets.

VALUES
Values Icon

Core Values

  • ✓ Quality First Approach
  • ✓ Farmer Empowerment
  • ✓ Sustainable Practices
  • ✓ Global Integrity
0
Partner Farms
0
Countries Served
0
Quality Score
Our Advantages

Why Choose Hembird

Quality Certified

ISO, HACCP, and FSSC 22000 certified facilities ensuring international quality standards

01

Sustainable Sourcing

Direct partnerships with farmers using ethical and sustainable Dehydrated practices

02

R&D Focused

Dedicated research team constantly improving products and processes

03

Global Reach

Established logistics network delivering to 25+ countries efficiently

04
5+
Years Experience
500+
Happy Clients
98%
Quality Score
24/7
Support
Our Capabilities

World-Class Infrastructure

State-of-the-art facilities designed to meet global standards while ensuring quality, efficiency, and sustainability

Manufacturing

Advanced Processing Units

  • 50,000 sq ft production area
  • Automated sorting & grading systems
  • Precision dehydration technology
  • Hygienic stainless steel equipment
5
Production Lines
24/7
Operations
Quality Control

Quality Assurance Labs

  • In-house microbiological testing
  • HPLC & GC analysis equipment
  • Metal detection systems
  • Certified quality analysts
100%
Batch Testing
12
QC Parameters
Storage

Modern Warehousing

  • Temperature-controlled storage
  • 100,000 sq ft capacity
  • FIFO inventory management
  • Pest-controlled environment
5000+
MT Capacity
24°C
Controlled Temp
Logistics

Efficient Logistics

  • In-house fleet of refrigerated trucks
  • Container loading facilities
  • Automated tracking systems
  • Customs clearance support
25+
Countries Served
48h
Dispatch Time
WhatsApp